PTFE film is an important engineering material for applications involving elevated temperatures, electrical insulation, chemical exposure, low-friction surfaces, and industrial release systems. Its distinctive fluoropolymer chemistry makes it useful in environments where conventional polymer films may experience adhesion, chemical attack, or thermal degradation.
However, selecting PTFE film requires more than identifying a nominal temperature rating. Engineers must consider film construction, thickness, dimensional stability, creep, electrical performance, surface treatment, processing conditions, and the actual operating environment.
A skived PTFE film, a cast PTFE film, and an adhesive-backed PTFE film may behave differently even when they share the same polymer designation.
This guide explains the engineering properties of PTFE film, its temperature limitations, common industrial applications, material comparisons, qualification methods, and practical purchasing requirements.
What Is PTFE Film?
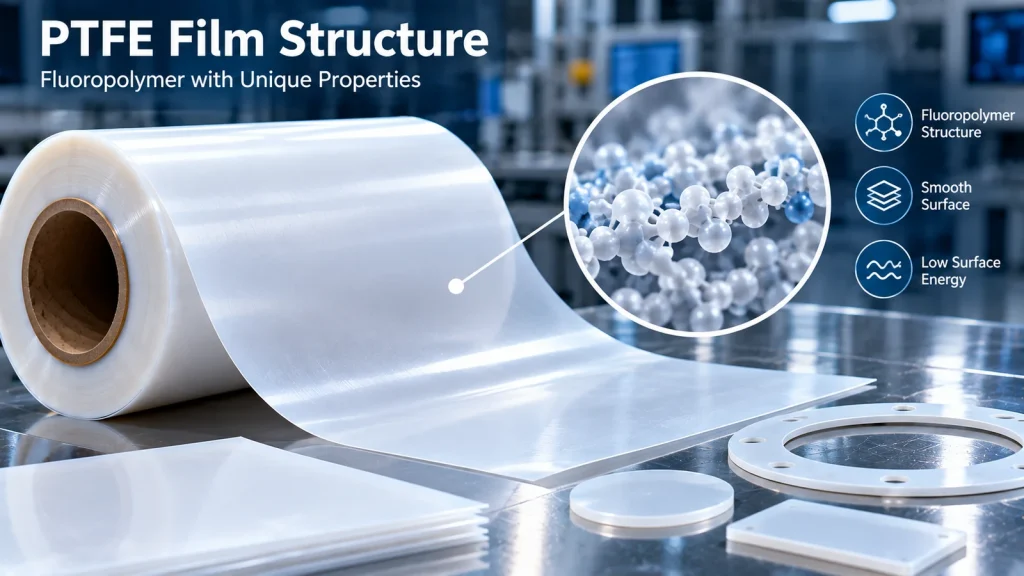
Polytetrafluoroethylene (PTFE) is a fluoropolymer consisting of a carbon-based polymer backbone surrounded by fluorine atoms.
The strong carbon–fluorine bonding and the polymer’s molecular structure contribute to PTFE’s chemical stability, low surface energy, electrical insulation properties, and resistance to elevated temperatures.
PTFE is commonly associated with:
- Thermal resistance in demanding industrial environments
- Chemical resistance against many aggressive substances
- Low surface energy and non-stick behavior
- Low friction against compatible counterfaces
- Electrical insulation and dielectric performance
- Resistance to moisture absorption
- Weathering and environmental durability
These properties make PTFE useful for industrial film constructions, release layers, electrical barriers, and specialized converting applications.
Nevertheless, PTFE is not a universal replacement for other high-performance films.
It can exhibit significant creep under sustained loading, relatively high thermal expansion, difficult adhesive bonding, and dimensional changes during thermal cycling.
Its mechanical performance must therefore be considered alongside its chemical and thermal advantages.
PTFE Film vs. PTFE Sheet
The distinction between PTFE film and PTFE sheet is often based on product thickness, flexibility, manufacturing method, and intended use rather than a universal industry thickness boundary.
Thin PTFE film is typically selected for wrapping, insulating, release, laminating, or precision-converted components.
Thicker PTFE sheet may be selected for gaskets, mechanical barriers, machined parts, or structural separation applications.
Purchasers should specify thickness, tolerance, manufacturing method, and delivery format instead of relying only on the terms “film” or “sheet.”
PTFE Film Temperature Resistance
Temperature resistance is one of the most important reasons engineers evaluate PTFE film.
Commercial PTFE film grades are frequently associated with maximum operating temperatures around 260°C (500°F). However, this figure is not a universal guaranteed service rating for every PTFE film, adhesive construction, or finished component.
For example, published technical literature for specific skived PTFE film grades identifies maximum operating temperatures of 260°C. That information applies to the referenced commercial products and must not be interpreted as a verified rating for all PTFE films supplied by other manufacturers.
Actual suitability depends on the selected grade, operating environment, exposure duration, applied load, dimensional tolerances, and applicable safety requirements.
Continuous Operating Temperature vs. Short-Term Peak Temperature
Engineers should distinguish between three thermal conditions.
Continuous service temperature describes the temperature at which a material must maintain required performance during prolonged operation.
Intermittent operating temperature describes repeated or occasional exposure during normal use.
Short-term peak temperature describes temporary thermal excursions, such as those encountered during manufacturing or abnormal operating events.
These conditions cannot be evaluated using temperature alone.
A PTFE film that remains physically intact after a brief heating cycle may still undergo creep, deformation, dimensional change, or deterioration of an associated adhesive system.
A complete thermal specification should include:
- Maximum and minimum temperatures
- Exposure duration
- Heating and cooling rates
- Number of thermal cycles
- Mechanical loading during exposure
- Required electrical performance
- Dimensional tolerance after exposure
- Contact materials and processing atmosphere
Thermal Expansion and Dimensional Stability
PTFE generally has a relatively high coefficient of thermal expansion compared with many dimensionally stable engineering films.
In precision assemblies, this can create movement between the PTFE layer and adjacent materials.
Potential consequences include:
- Misalignment of die-cut features
- Wrinkling in constrained laminates
- Loss of dimensional registration
- Localized stress near fasteners or bonded interfaces
- Changes in gasket or separator geometry
Dimensional behavior can also depend on previous thermal history and manufacturing conditions.
For applications involving repeated heating, evaluate the actual film construction through representative thermal cycling tests.
Thermal Decomposition and Processing Safety
PTFE’s thermal resistance does not mean it can be heated without limits.
Excessive temperatures can cause thermal decomposition and the release of hazardous fumes.
Processing conditions should remain within the limits established by the applicable supplier’s safety documentation and process requirements.
Industrial heating equipment should use appropriate temperature controls, ventilation, and safety procedures.
The melting transition of PTFE must not be confused with its allowable continuous service temperature.
Thermal Selection Checklist
Before approving PTFE film for an elevated-temperature application, confirm:
- The actual temperature profile.
- The duration and frequency of thermal exposure.
- Whether the film is mechanically constrained.
- Whether the application requires dimensional precision.
- Whether adhesives, coatings, or other layers are present.
- Whether electrical properties must be retained after aging.
- The film supplier’s grade-specific thermal documentation.
Key Mechanical and Physical Properties of PTFE Film
Tensile Strength and Elongation
PTFE film can provide useful flexibility and elongation, but its mechanical properties vary with resin formulation, processing method, film thickness, and testing direction.
Tensile strength and elongation should be evaluated using grade-specific data.
For thin films, ASTM D882 may be relevant when the specimen and material construction fall within the method’s scope.
Important factors include:
- Tensile strength at the operating temperature
- Elongation at break
- Tear propagation
- Handling damage during converting
- Direction-dependent mechanical behavior
- Film defects and thickness variation
Room-temperature tensile performance alone may not predict performance under prolonged thermal loading.
Creep and Cold Flow
PTFE can deform gradually when subjected to sustained stress.
This behavior is commonly described as creep or cold flow.
For insulating spacers, compression-loaded barriers, and gasket-like components, creep may reduce dimensional stability or contact pressure.
Engineers should evaluate long-term deformation under the actual combination of temperature, pressure, and exposure time.
Where mechanical load retention is essential, another material or a reinforced construction may be more appropriate.
Thickness and Tolerance
Film thickness affects handling, flexibility, dielectric performance, mechanical strength, and converting precision.
Nominal thickness is only the starting point.
Critical specifications may include:
- Thickness tolerance
- Cross-web thickness variation
- Width tolerance
- Roll length
- Flatness
- Edge quality
- Surface defects
- Winding tension
- Core and packaging requirements
For precision die-cut parts, thickness consistency may be as important as the nominal gauge.
PTFE Film Electrical Insulation Properties
PTFE film is used in selected electrical insulation applications because of its dielectric characteristics, high electrical resistivity, and performance across demanding environments.
Potential uses include insulating barriers, cable constructions, transformer spacers, and specialized electronic assemblies.
Dielectric Strength
Dielectric strength describes the electric field at which a material breaks down under specified test conditions.
It is influenced by:
- Film thickness
- Material defects
- Electrode geometry
- Voltage waveform
- Test temperature
- Moisture and contamination
- Test duration
- Test environment
ASTM D149 is a commonly used method for dielectric breakdown testing of solid electrical insulating materials.
A reported dielectric strength value should not be treated as a universal design limit.
Dielectric Constant and Dissipation Factor
PTFE is frequently considered for high-frequency electrical applications because of its dielectric behavior.
However, dielectric constant and dissipation factor must be evaluated at the relevant frequency and temperature.
For RF and microwave-related applications, engineers should also consider dimensional stability, laminate construction, bonding compatibility, and the electrical characteristics of the complete assembly.
Electrical Aging and Insulation-System Qualification
The long-term electrical suitability of PTFE film depends on the complete operating environment.
Temperature, electrical stress, contamination, and mechanical damage can affect the performance of the insulation system.
A material’s generic electrical properties do not establish compliance with a particular equipment standard.
Specific UL recognition, flame classification, thermal class, or other certification must be confirmed for the exact commercial grade and applicable construction.
Chemical Resistance, Surface Energy, and Low-Friction Behavior
Chemical Resistance
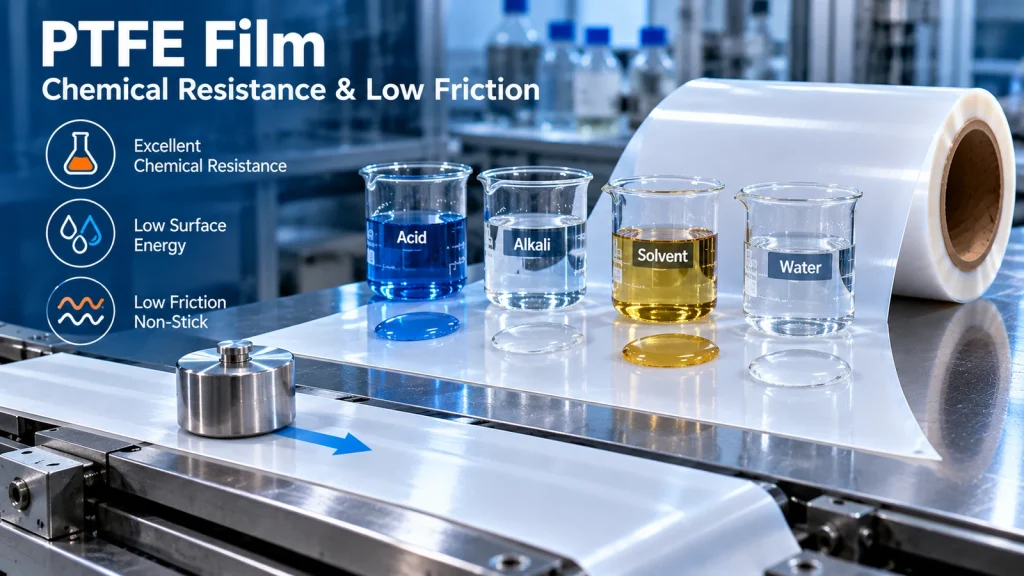
PTFE is highly resistant to many industrial chemicals, making it useful in chemical-processing and contamination-sensitive environments.
Nevertheless, chemical compatibility should not be assumed for every substance or operating condition.
Compatibility depends on:
- Chemical identity
- Concentration
- Temperature
- Exposure duration
- Mechanical stress
- Film purity and formulation
- Presence of adhesives or coatings
The compatibility of the finished assembly may be limited by materials other than PTFE.
For critical chemical applications, evaluate the complete construction rather than the polymer substrate alone.
Low Surface Energy and Release Performance
PTFE has low surface energy, which contributes to its non-stick characteristics.
This can be advantageous in release layers, process separators, and applications where adhesion to contacting materials must be minimized.
However, release behavior also depends on surface finish, contact pressure, temperature, contamination, and the chemistry of the contacting material.
PTFE film should not automatically be considered suitable for every resin, adhesive, or thermal press process.
Friction and Wear
PTFE can provide low friction against suitable counterfaces.
Nevertheless, low friction does not necessarily imply high wear resistance.
Unfilled PTFE may experience wear, deformation, or creep under demanding mechanical conditions.
For moving components, evaluate contact pressure, sliding speed, surface finish, temperature, and expected service life.
Bonding and Surface Treatment
Untreated PTFE is difficult to bond using many conventional adhesives because of its low surface energy.
Specialized surface treatments, such as chemical etching or other qualified surface modification processes, may be used to improve adhesion.
Surface treatment must be matched to the adhesive, substrate, operating environment, and required bond durability.
Do not assume untreated and treated PTFE films are interchangeable.
PTFE Film Types and Manufacturing Methods
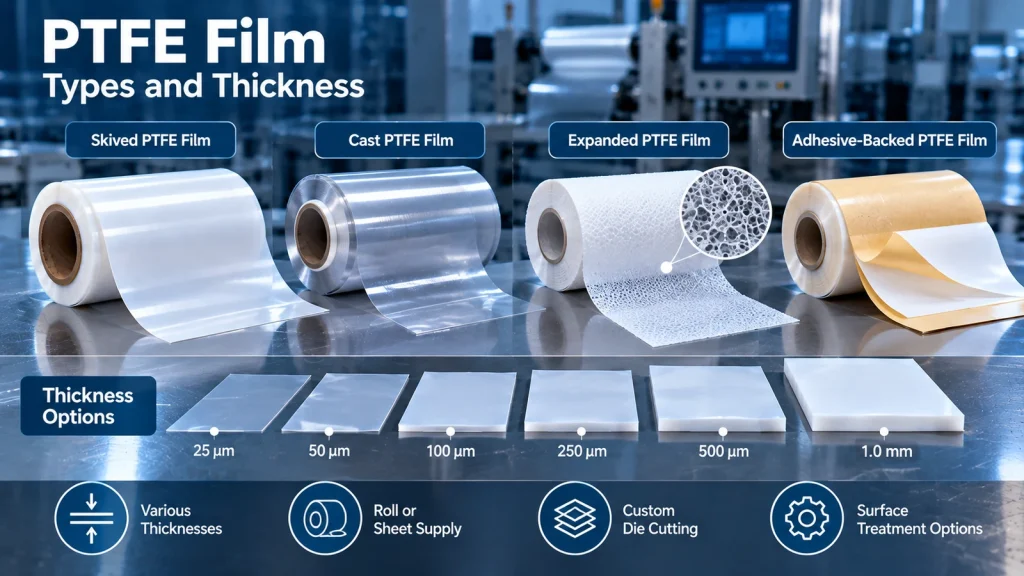
PTFE films are available in different constructions and manufacturing forms.
Skived PTFE Film
Skived PTFE film is commonly produced by slicing thin layers from a processed PTFE billet.
It is widely used in electrical insulation, mechanical separation, release applications, and specialized converting.
Relevant selection factors include thickness tolerance, surface finish, dimensional consistency, and handling characteristics.
Cast PTFE Film
Certain PTFE film constructions are produced through dispersion-based coating or casting processes.
These films may differ from skived products in construction, thickness range, surface characteristics, and processing behavior.
The manufacturing method should be verified for the exact commercial product.
Expanded PTFE Film
Expanded PTFE, commonly abbreviated ePTFE, has a porous microstructure.
Its properties and intended applications can differ significantly from dense, nonporous PTFE film.
ePTFE should not be substituted for dense PTFE film without confirming porosity, permeability, mechanical properties, and electrical suitability.
Adhesive-Backed PTFE Film
PTFE film may be supplied as part of an adhesive tape construction.
In such products, the adhesive can impose a lower service-temperature limit than the PTFE backing.
Engineers must evaluate:
- PTFE backing thickness
- Total tape thickness
- Adhesive chemistry
- Peel adhesion
- Shear performance
- Thermal aging
- Chemical compatibility
- Release liner and converting requirements
A PTFE film tape should never be evaluated using the backing’s properties alone.
PTFE Film vs. PET, PI, PEN, FEP, and PFA
Selecting the best industrial film requires comparing the properties that matter to the finished application.
| Material | Potential Advantages | Main Limitations | Common Selection Drivers |
|---|---|---|---|
| PTFE | Chemical resistance, low surface energy, electrical insulation, elevated-temperature capability | Creep, thermal expansion, difficult bonding | Release layers, chemical barriers, specialized electrical insulation |
| PET | Dimensional stability, mechanical strength, converting versatility | Lower high-temperature capability than PTFE or many PI grades | Electrical insulation, printed films, die-cut components |
| PI | High-temperature performance, mechanical integrity, electrical insulation | Grade-dependent chemical and moisture behavior, higher cost | High-temperature electronic insulation |
| PEN | Potentially improved thermal and dimensional performance compared with conventional PET | Cost and grade-dependent availability | Precision electrical and electronic films |
| FEP | Fluoropolymer chemical resistance and thermoplastic melt-processing characteristics | Different temperature and mechanical limits from PTFE | Heat-sealable fluoropolymer films and insulation |
| PFA | High chemical resistance and thermoplastic processing capability | Cost and application-specific limitations | Chemical and high-temperature film constructions |
These comparisons are qualitative. Actual performance must be confirmed using commercial-grade technical data.
When Should Engineers Choose PTFE Instead of Polyimide?
PTFE may be preferable when low surface energy, chemical resistance, or non-stick behavior is the primary requirement.
Polyimide may be preferable where dimensional stability, mechanical integrity, and demanding electronic insulation performance are more important.
Neither material should be selected based on temperature rating alone.
When Is FEP or PFA More Appropriate?
FEP and PFA may be evaluated when melt-processability, heat sealing, or particular fabrication requirements are important.
The selection should consider processing temperature, dielectric performance, chemical exposure, dimensional tolerance, and total system cost.
Industrial Applications of PTFE Film
1. Electrical Insulation and Cable Assemblies
PTFE film may be used in selected electrical insulation constructions, wire and cable systems, spacers, and barriers.
Important specifications include dielectric performance, thickness uniformity, temperature exposure, and long-term reliability.
2. PCB and Electronics Manufacturing
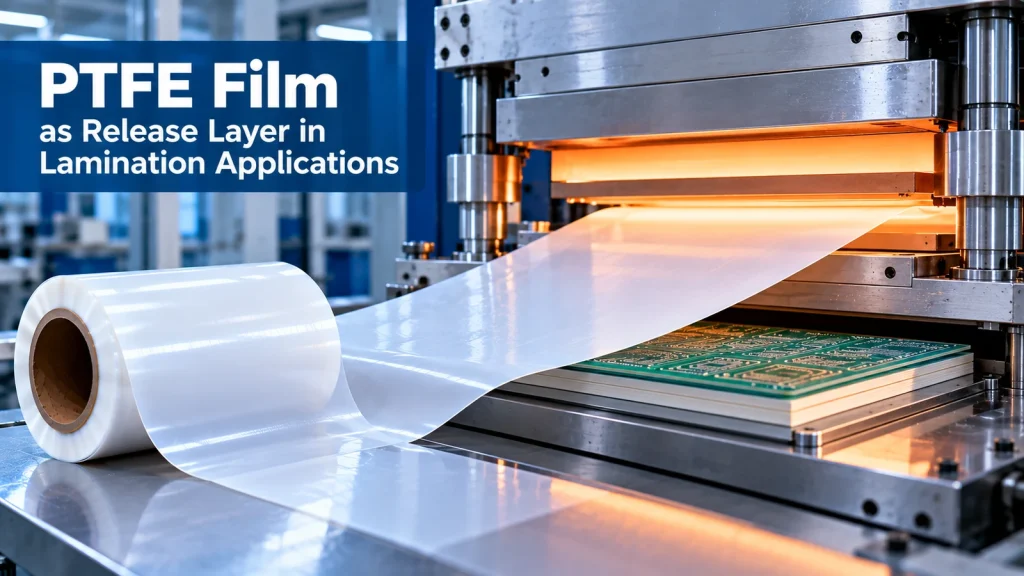
PTFE film may be evaluated for release, separation, or insulating functions in selected electronics manufacturing processes.
For PCB lamination or thermal pressing, engineers should confirm that the film can withstand the actual pressure, temperature, cycle time, and contact materials.
A generic PTFE film should not automatically be treated as a qualified PCB lamination release material.
3. Semiconductor and Precision Electronics
PTFE may be considered where chemical compatibility, electrical insulation, or low adhesion is important.
However, semiconductor-related applications may require strict control of ionic contamination, particles, extractables, and cleanliness.
General industrial PTFE film is not automatically suitable for cleanroom or semiconductor-contact use.
4. Battery and Energy Storage Manufacturing
PTFE film may be considered for selected auxiliary insulating, release, or processing components.
Battery applications require careful evaluation of thermal conditions, electrical isolation, mechanical stresses, and chemical exposure.
PTFE film should not be described as a qualified battery separator or safety barrier without application-specific validation.
5. Composite Processing and Mold Release
PTFE film can be evaluated as a release or separation layer in selected composite manufacturing operations.
Selection depends on resin chemistry, curing temperature, pressure, surface finish, and desired release characteristics.
6. Precision Die-Cut Components
PTFE film may be converted into custom shapes for insulating barriers, spacers, sliding interfaces, and process components.
Converting considerations include:
- Material handling
- Edge quality
- Dimensional tolerance
- Static control
- Part distortion
- Surface cleanliness
- Packaging and traceability
7. Chemical Processing and Industrial Equipment
PTFE film may be used as a protective, insulating, or separating layer where chemical exposure is important.
Mechanical load, abrasion, creep, and operating temperature must be evaluated alongside chemical resistance.
Common PTFE Film Selection Mistakes
Mistake 1: Treating 260°C as a Universal Guaranteed Rating
Published ratings apply to specific materials and test conditions.
Prevention: Request grade-specific thermal documentation and validate the actual operating cycle.
Mistake 2: Ignoring Creep Under Load
PTFE may deform during prolonged compression or mechanical loading.
Prevention: Evaluate long-term deformation at the intended temperature and stress.
Mistake 3: Assuming PTFE Is Easy to Bond
Untreated PTFE can be difficult to bond.
Prevention: Confirm surface treatment and validate the adhesive system.
Mistake 4: Confusing PTFE Film with PTFE Adhesive Tape
The backing and adhesive can have different thermal, chemical, and electrical limitations.
Prevention: Evaluate the entire tape construction.
Mistake 5: Ignoring Thermal Expansion
Dimensional changes may create assembly stress or misalignment.
Prevention: Conduct thermal cycling and dimensional inspection.
Mistake 6: Selecting Only by Nominal Thickness
Different films may have different thickness tolerances, defects, and mechanical properties.
Prevention: Specify measurable acceptance criteria and conduct sample qualification.
Mistake 7: Assuming All PTFE Grades Have the Same Cleanliness
Particle, ionic, and extractable requirements can vary considerably by application.
Prevention: Specify cleanliness criteria and request relevant documentation.
Failure Risks and Prevention
| Failure Mode | Potential Cause | Preventive Action |
|---|---|---|
| Creep or deformation | Sustained load, elevated temperature | Compression and creep testing |
| Dimensional instability | Thermal expansion or process history | Thermal cycling and dimensional measurement |
| Adhesive delamination | Low surface energy, incompatible adhesive | Surface treatment and bond testing |
| Electrical breakdown | Defects, contamination, inadequate insulation design | Dielectric and environmental testing |
| Surface damage | Improper handling or converting | Inspection and handling controls |
| Premature tape failure | Adhesive limitations | Validate complete adhesive construction |
| Chemical-related failure | Incompatible assembly materials | Full-system compatibility testing |
Recommended Testing and Validation
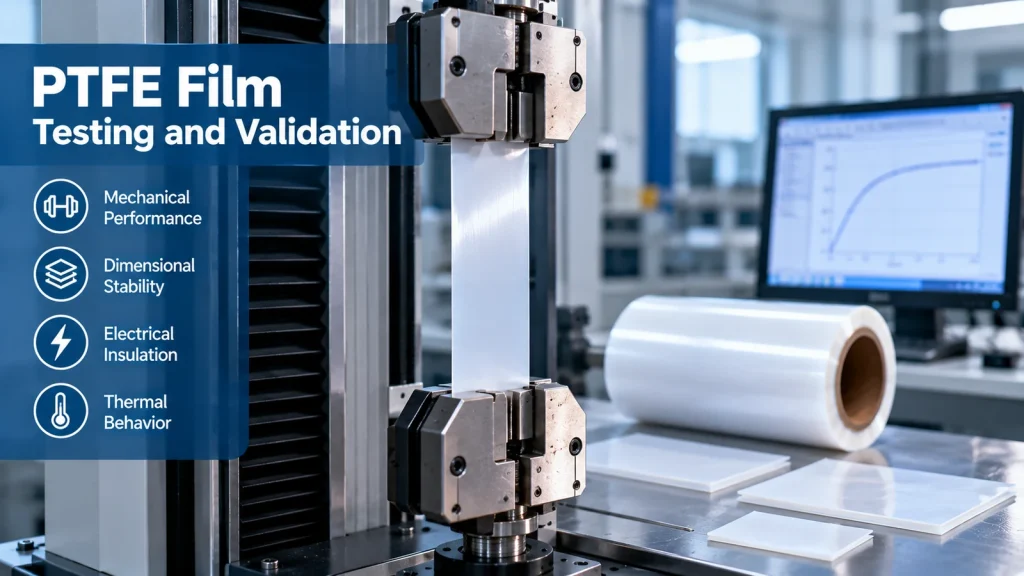
A reliable material qualification plan should reflect the finished application’s critical requirements.
| Property | Potential Test Method | Purpose |
|---|---|---|
| Thickness | ASTM D374 or suitable calibrated method | Confirm film thickness |
| Tensile properties | ASTM D882 where applicable | Evaluate strength and elongation |
| Dielectric breakdown | ASTM D149 | Assess electrical insulation behavior |
| Density | ASTM D792 where applicable | Support material characterization |
| Thermal dimensional change | Defined heat-exposure and dimensional measurement procedure | Evaluate expansion or shrinkage |
| Creep | Application-specific sustained-load test | Evaluate long-term deformation |
| Chemical compatibility | Controlled exposure and post-exposure inspection | Evaluate chemical effects |
| Bond strength | Suitable peel or adhesion test | Validate treated or bonded constructions |
| Surface condition | Visual, microscopic, or cleanliness inspection | Identify defects and contamination |
ASTM D3308 may also be relevant to certain PTFE resin skived-tape specifications, while ASTM D3369 addresses PTFE fluoropolymer resin cast film. Their applicability must be checked against the actual product and purchasing specification.
Sample Qualification Procedure
A practical evaluation process may include:
- Review the material’s TDS and available safety documentation.
- Inspect sample thickness, appearance, and surface condition.
- Test critical properties under representative conditions.
- Conduct thermal and mechanical aging where required.
- Evaluate performance after environmental exposure.
- Test compatibility with adjacent materials.
- Conduct a production-representative converting or assembly trial.
- Establish measurable acceptance criteria before production approval.
For electrical safety applications, qualification should be aligned with the applicable equipment and insulation-system requirements.
Step-by-Step PTFE Film Selection Guide
Step 1 — Identify the film’s function.
Determine whether PTFE will act as an electrical insulator, release layer, chemical barrier, low-friction surface, or converted component.
Step 2 — Define the operating environment.
Record continuous temperature, peak temperature, pressure, chemical exposure, electrical stress, and expected service life.
Step 3 — Choose the construction.
Evaluate skived, cast, expanded, surface-treated, or adhesive-backed PTFE according to the required function.
Step 4 — Specify dimensions.
Define thickness, tolerance, width, roll length, sheet size, or finished-part geometry.
Step 5 — Identify critical material properties.
Determine which properties require numerical acceptance criteria and test documentation.
Step 6 — Evaluate manufacturing compatibility.
Review slitting, die cutting, lamination, bonding, handling, and packaging requirements.
Step 7 — Request samples and technical documentation.
Verify the proposed grade against the application specification.
Step 8 — Approve the qualified material.
Document the approved grade, critical properties, supplier requirements, and change-control conditions.
PTFE Film RFQ Checklist
For efficient technical evaluation and sourcing, provide the following information:
| RFQ Item | Required Information |
|---|---|
| Material | PTFE film type or reference grade |
| Application | Electrical insulation, release, chemical barrier, die cutting, or other |
| Temperature | Continuous, intermittent, and peak exposure |
| Electrical requirements | Voltage, dielectric testing, relevant standards |
| Thickness | Nominal thickness and tolerance |
| Dimensions | Roll width, roll length, sheet size, or finished part |
| Drawings | 2D/3D drawings and dimensional tolerances if applicable |
| Surface | Untreated, treated, or adhesive-backed requirements |
| Mechanical requirements | Load, creep, flexibility, and handling requirements |
| Chemical exposure | Chemicals, concentrations, temperature, and duration |
| Documentation | TDS, test reports, compliance documents, traceability |
| Quantity | Prototype quantity, order quantity, and annual demand |
| Logistics | Delivery destination and required schedule |
A complete RFQ allows potential suppliers to evaluate technical compatibility before confirming commercial availability.
Frequently Asked Questions
1. What is PTFE film used for?
PTFE film is used in selected electrical insulation, industrial release, chemical-resistant, low-friction, and precision-converted applications. Suitability depends on the specific film construction and operating conditions.
2. What is the maximum temperature resistance of PTFE film?
Certain commercial PTFE film grades publish maximum operating temperatures around 260°C. This is not a universal rating. Continuous service suitability must be confirmed for the exact grade and application.
3. Is PTFE film suitable for electrical insulation?
PTFE film is used in electrical insulation applications, but dielectric performance, thickness, aging, and applicable safety requirements must be verified.
4. What is the difference between skived PTFE film and cast PTFE film?
Skived film is typically produced by slicing processed PTFE material, while cast-film constructions use different manufacturing methods. Their thickness ranges, surface characteristics, and mechanical behavior may differ.
5. Can PTFE film be die cut?
PTFE film can be die cut, but dimensional accuracy and edge quality depend on film thickness, tooling, handling, and material behavior.
6. Does PTFE film shrink or expand when heated?
PTFE can undergo significant dimensional change with temperature. Its thermal expansion and processing history must be considered in precision applications.
7. Can PTFE film be bonded with adhesive?
Untreated PTFE is difficult to bond using many conventional adhesives. Surface treatment or specialized bonding systems may be required.
8. Is PTFE film better than polyimide film?
Neither material is universally better. PTFE may offer advantages in chemical resistance and release behavior, while polyimide may be preferable for certain mechanically demanding high-temperature electronic applications.
9. Is PTFE film the same as PTFE tape?
Not necessarily. PTFE tape may refer to unsupported film or an adhesive-backed construction. Adhesive-backed products must be evaluated as complete systems.
10. What information is needed to request a PTFE film quotation?
Provide the application, temperature profile, electrical requirements, film type, thickness, dimensions, drawings, test standards, and expected purchasing quantity.
Request PTFE Film for Your Industrial Application
Choosing PTFE film requires balancing temperature resistance, electrical performance, chemical compatibility, mechanical stability, and manufacturing requirements.
HighTemp Material welcomes technical inquiries for industrial polymer films and related material selection.
If you are evaluating PTFE film for electronics manufacturing, electrical insulation, industrial release, or precision-converted components, share your specifications so the appropriate material requirements can be reviewed.
Request a PTFE Film Quote
Please include:
- Material type or reference grade
- Intended application
- Continuous and peak temperatures
- Electrical requirements
- Required thickness and dimensions
- Drawings or converting specifications
- Relevant test standards
- Estimated order quantity and annual demand
Visit https://www.hightempmaterial.com/ to contact HighTemp Material.
Material availability, grade-specific properties, certifications, and custom processing capabilities must be confirmed before quotation or production approval.