An Engineering Guide to Adhesion Loss, Residue, Cohesive Failure, Thermal Degradation and Tape Reliability
High-temperature adhesive tapes are widely used in PCB and SMT manufacturing, electrical insulation, powder coating, composite processing, battery assembly and industrial masking.
However, a tape described as “high temperature” does not necessarily perform reliably in every elevated-temperature application.
One tape may lift from a metal surface during heating. Another may remain firmly bonded but leave adhesive residue after removal. A third may become brittle after repeated thermal exposure, even though its initial adhesion was acceptable.
These failures have different causes and require different solutions.
For engineers and technical buyers, the most important question is not simply:
“What temperature can this tape withstand?”
It is:
“Will the complete tape construction maintain the required adhesion, mechanical integrity and removal performance under the actual process or service conditions?”
This guide explains six common failure modes of high-temperature adhesive tapes, how to distinguish them, which testing methods are useful and how to reduce failure risk when selecting polyimide, polyester, PTFE-based and other industrial tape constructions.
1. Why High-Temperature Adhesive Tapes Fail
An adhesive tape is a multilayer construction rather than a single material.
Depending on the product, it may contain:
- A polymer film or reinforced backing
- A pressure-sensitive adhesive (PSA)
- A primer or surface treatment
- A release liner
- Additional coatings or functional layers
The tape is then applied to another material, such as aluminum, stainless steel, copper, glass, a PCB surface or a coated component.
Each layer and interface can behave differently when exposed to heat.
Temperature Resistance Is Not a Single Property
A backing may tolerate a temperature that exceeds the usable limit of its adhesive.
Similarly, an adhesive may retain some bonding capability after heating but become difficult to remove cleanly.
The relevant performance depends on:
- Continuous versus short-term peak temperature
- Heating duration
- Number of thermal cycles
- Substrate chemistry and surface condition
- Applied pressure and bonding time
- Peel, shear and mechanical loading
- Removal temperature and method
- Exposure to oils, solvents or cleaning chemicals
A published temperature rating should therefore be interpreted together with its test conditions and performance criteria.
Temporary Masking vs Permanent Bonding
These applications have different requirements.
Temporary masking tapes must often remain in position during processing and then remove without unacceptable residue or surface damage.
Permanent insulation tapes may need to retain adhesion and electrical insulation properties throughout the intended service life.
A tape optimized for strong long-term adhesion may not be suitable for clean removal after a high-temperature process.
Likewise, a removable masking tape may not be appropriate for a permanent structural or electrical bonding application.
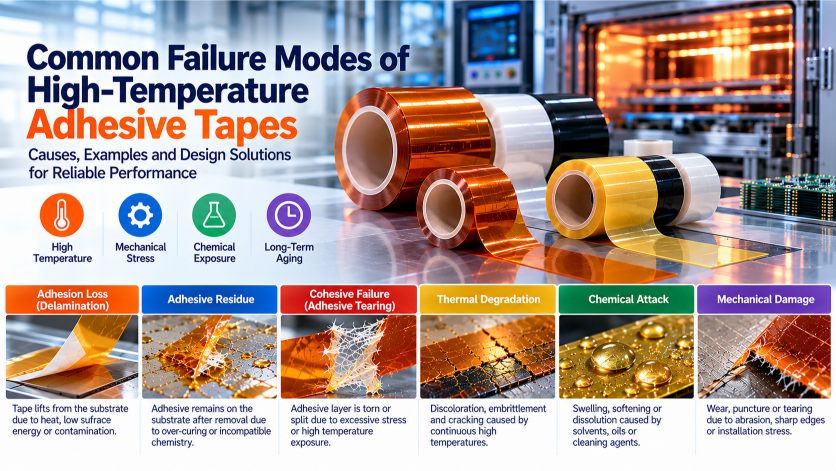
2. Overview of Common High-Temperature Tape Failure Modes
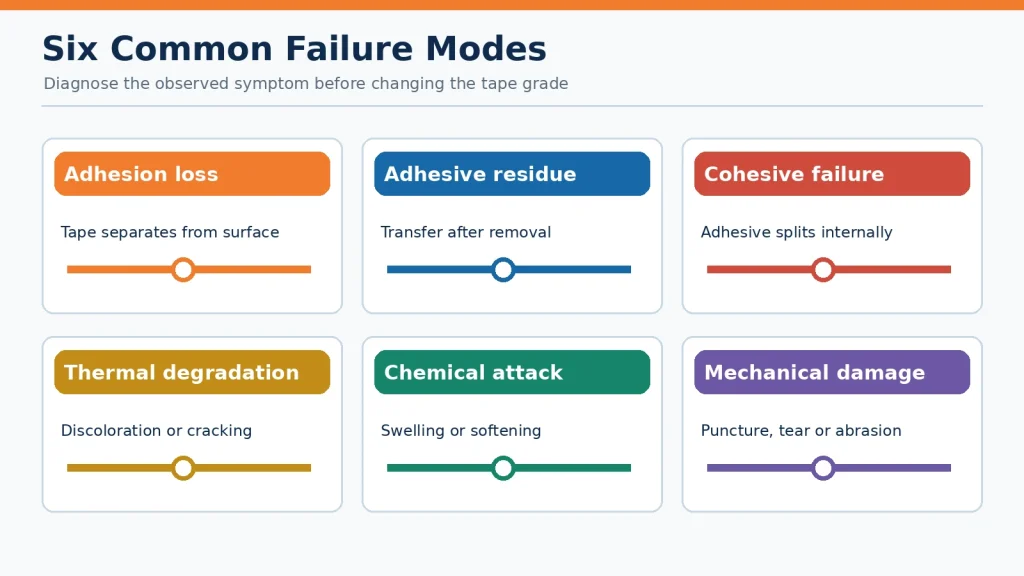
The first step in troubleshooting is identifying where and how the failure occurred.
| Failure Mode | Typical Symptom | Primary Investigation |
|---|---|---|
| Adhesion loss | Tape lifts or separates from substrate | Interface adhesion and surface condition |
| Adhesive residue | Adhesive remains after tape removal | Adhesive stability and removal conditions |
| Cohesive failure | Adhesive splits within its own layer | Internal adhesive strength |
| Thermal degradation | Discoloration, cracking or embrittlement | Heat exposure and material aging |
| Chemical attack | Swelling, softening or property changes | Chemical compatibility |
| Mechanical damage | Tearing, puncture or abrasion | Backing strength and installation geometry |
These failure modes can occur together.
For example, heat aging may weaken an adhesive, which then experiences cohesive failure during removal.
A contaminated substrate may cause adhesion loss even when the tape itself remains chemically stable.
Correct diagnosis requires identifying the failed layer or interface—not simply observing that the tape no longer works.
3. Adhesion Loss and Delamination
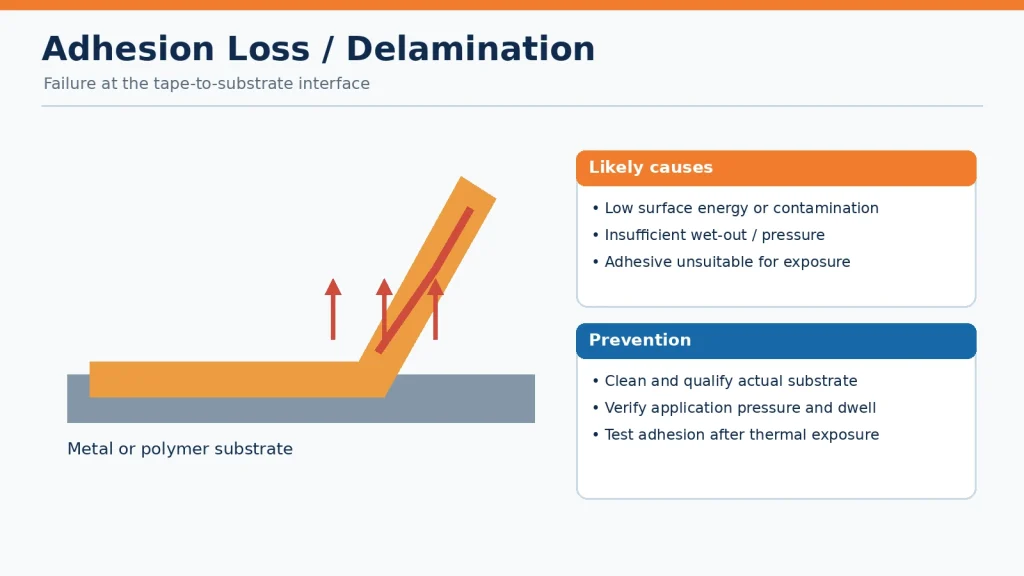
Adhesion loss occurs when a tape separates from the surface to which it was applied.
The failure may begin at an edge, around a hole or along a curved surface.
Typical Symptoms
- Tape edge lifting during heating
- Partial or complete detachment
- Bubbles beneath the tape
- Reduced adhesion after thermal cycling
- Poor bonding to certain coated or polymer surfaces
Common Root Causes
Low surface energy
Some materials, including untreated PTFE and certain silicone-containing surfaces, are difficult to bond with conventional adhesives.
Low surface energy can limit adhesive wetting and intimate contact.
Surface contamination
Oil, dust, release agents, fingerprints and processing residues can interfere with bonding.
Insufficient application pressure or dwell
Pressure-sensitive adhesives generally require appropriate contact pressure and time to develop adhesion.
Thermal expansion mismatch
Different expansion rates between tape and substrate can create interface stress during heating and cooling.
Incorrect adhesive selection
An adhesive may not maintain adequate performance at the actual operating temperature or on the specified substrate.
Prevention Strategies
- Identify the actual substrate and surface finish.
- Establish a suitable cleaning and surface preparation procedure.
- Verify the adhesive’s compatibility with the substrate.
- Control application pressure, temperature and dwell time.
- Evaluate adhesion after representative thermal exposure.
- Consider edge geometry and mechanical constraints.
Surface treatments such as plasma or primers may improve bonding in some systems, but they must be validated for the actual materials and process.
Useful Tests
Peel adhesion testing can help compare adhesive constructions.
ASTM D3330/D3330M is a commonly referenced method for pressure-sensitive tape peel adhesion.
However, test angle, peel rate, substrate, dwell time and temperature must be reported.
4. Adhesive Residue After High-Temperature Removal
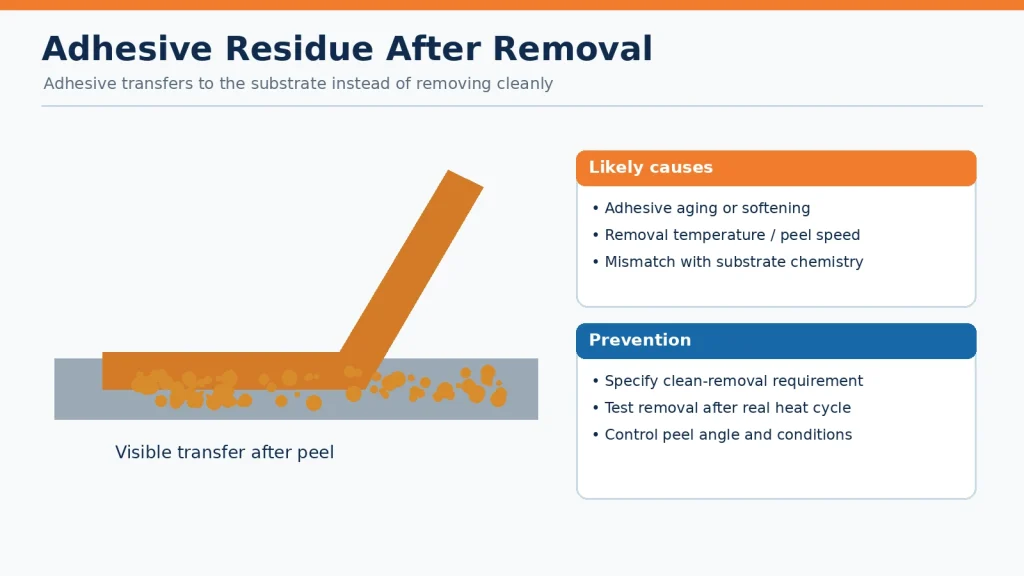
Adhesive residue occurs when part of the adhesive remains on the substrate after tape removal.
For temporary masking applications, this can be a critical failure because it may require cleaning, rework or component rejection.
Typical Symptoms
- Sticky deposits on metal or glass
- Visible adhesive transfer
- Residue after oven exposure
- Difficult removal from coated surfaces
- Contamination before a subsequent manufacturing step
Why Residue Occurs
Thermal aging of the adhesive
Prolonged heat exposure can change adhesive chemistry and mechanical properties.
Loss of cohesive strength
If the adhesive becomes too weak internally, it may split during removal.
Excessive bonding to the substrate
In some constructions, the adhesive-substrate bond may become stronger than the adhesive’s internal strength.
Inappropriate removal conditions
Removal temperature, peel angle and peel rate can influence residue formation.
Chemical interaction
The adhesive may interact with coatings, oils or other surface materials.
Prevention Strategies
For clean-removal applications:
- Specify the maximum process temperature and exposure duration.
- Request evidence of removal performance after the relevant process.
- Test on the actual coated or uncoated substrate.
- Evaluate removal at the intended temperature.
- Define acceptable residue and contamination limits.
- Compare adhesive formulations rather than selecting by backing material alone.
Important Distinction
A tape described as “silicone adhesive” is not automatically residue-free.
Likewise, an acrylic adhesive is not automatically unsuitable for elevated-temperature use.
The exact formulation, backing, substrate and test conditions determine performance.
Practical Manufacturing Example
A PCB masking tape may survive an oven process without lifting but leave adhesive transfer during removal.
In this case, higher initial peel adhesion may not solve the problem.
The engineer should investigate adhesive aging, cohesive strength and removal conditions.
5. Cohesive Failure: When the Adhesive Splits Internally
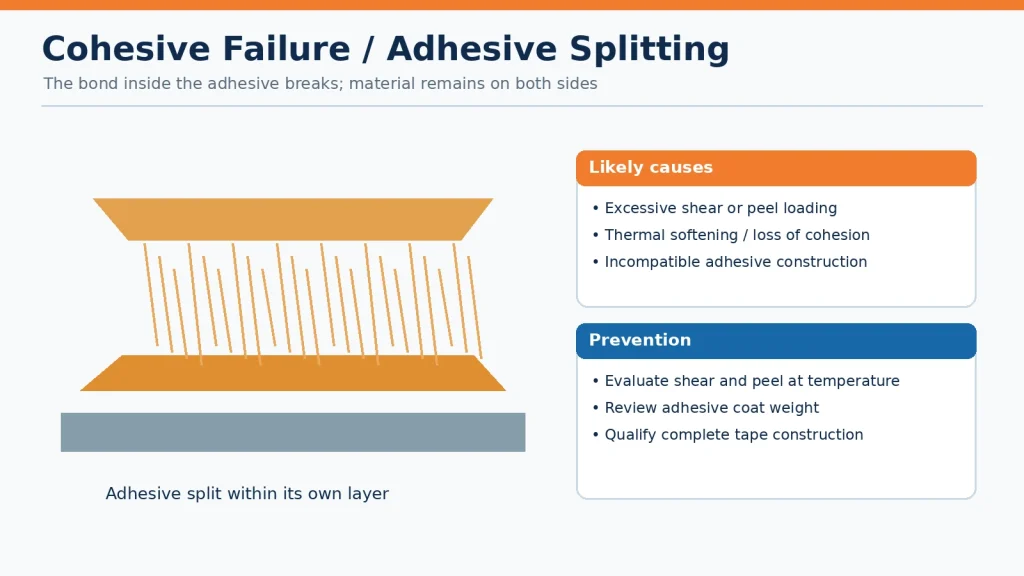
Cohesive failure occurs within the adhesive layer rather than at the adhesive-substrate interface.
During removal or mechanical loading, part of the adhesive may remain on each side of the separation.
Adhesive Failure vs Cohesive Failure
These terms describe different locations of failure.
Adhesive or interfacial failure: Separation occurs at the interface between two materials.
Cohesive failure: Separation occurs within the adhesive material itself.
The distinction is important because the corrective actions differ.
Common Causes
- Insufficient internal adhesive strength
- Excessive shear or peel stress
- High-temperature softening
- Long-term thermal aging
- Excessive adhesive thickness for the application
- Incompatible adhesive and backing construction
Why Adhesive Thickness Matters
Increasing adhesive coat weight may improve wetting or gap filling in some applications.
However, a thicker adhesive layer can also influence creep, deformation and cohesive failure.
More adhesive is not always better.
Prevention Strategies
- Compare adhesive cohesive strength at the relevant temperature.
- Evaluate shear holding power and creep.
- Review adhesive thickness and construction.
- Reduce unnecessary mechanical loading.
- Test the complete tape on the actual substrate.
ASTM D3654/D3654M is a relevant reference for shear adhesion of pressure-sensitive tapes.
The test configuration should reflect the actual loading conditions where possible.
6. Thermal Degradation, Discoloration and Embrittlement
Thermal degradation refers to changes in material properties caused by heat exposure.
Depending on the polymer and environment, prolonged heating may produce chemical aging, oxidation, physical changes or mechanical deterioration.
Typical Symptoms
- Discoloration
- Cracking
- Reduced flexibility
- Brittle backing
- Changes in adhesion
- Loss of elongation
- Difficulty removing the tape intact
Discoloration alone does not necessarily prove functional failure.
However, it may indicate that additional mechanical, adhesive or electrical testing is needed.
Continuous Temperature vs Peak Temperature
A tape may tolerate a short thermal excursion that would be unsuitable for prolonged exposure.
For example, a brief manufacturing process and continuous operation at the same nominal temperature represent different conditions.
Engineers should request both:
- Continuous service temperature information
- Short-duration or peak exposure information
The supporting test conditions are essential.
Backing and Adhesive Can Age Differently
A polyimide backing may remain mechanically intact while its adhesive loses required performance.
Conversely, an adhesive may retain bonding ability while the backing becomes brittle or cracks.
The complete construction must be evaluated.
Thermal Cycling Effects
Repeated heating and cooling can introduce expansion mismatch and mechanical stress.
Potential consequences include:
- Edge lifting
- Wrinkling
- Cracking
- Adhesive fatigue
- Dimensional changes
Thermal cycling performance cannot be established from a single static-temperature rating.
Prevention Strategies
- Select both backing and adhesive for the temperature profile.
- Confirm exposure duration and atmosphere.
- Conduct thermal aging and cycling tests where required.
- Measure peel, shear and mechanical properties after exposure.
- Evaluate changes in removal behavior.
- Avoid assuming that a higher backing temperature rating guarantees better tape performance.
7. Chemical Attack and Environmental Compatibility
High-temperature tapes may encounter cleaning solvents, process chemicals, oils, humidity or other contaminants.
Chemical exposure can affect either the adhesive or backing.
Typical Symptoms
- Swelling
- Softening
- Loss of adhesion
- Surface changes
- Adhesive transfer
- Cracking or embrittlement after exposure
Important Variables
Chemical compatibility depends on:
- Chemical identity
- Concentration
- Temperature
- Exposure duration
- Mechanical loading
- Adhesive formulation
- Backing material
A material that tolerates brief contact at room temperature may behave differently during prolonged exposure at elevated temperature.
PTFE and Chemical Resistance
PTFE is widely valued for chemical resistance.
However, a PTFE-based adhesive tape is not made entirely of PTFE.
Its adhesive, primer, reinforcement and other layers may have different chemical compatibility.
Therefore, chemical resistance of the backing does not establish compatibility of the complete tape.
Prevention Strategies
- Identify all process chemicals and cleaning agents.
- Request grade-specific chemical compatibility information.
- Test the complete tape construction.
- Evaluate exposure at representative temperatures.
- Inspect adhesive retention, swelling and removal behavior.
- Consider protective design changes when direct exposure cannot be avoided.
8. Mechanical Damage, Tearing and Abrasion
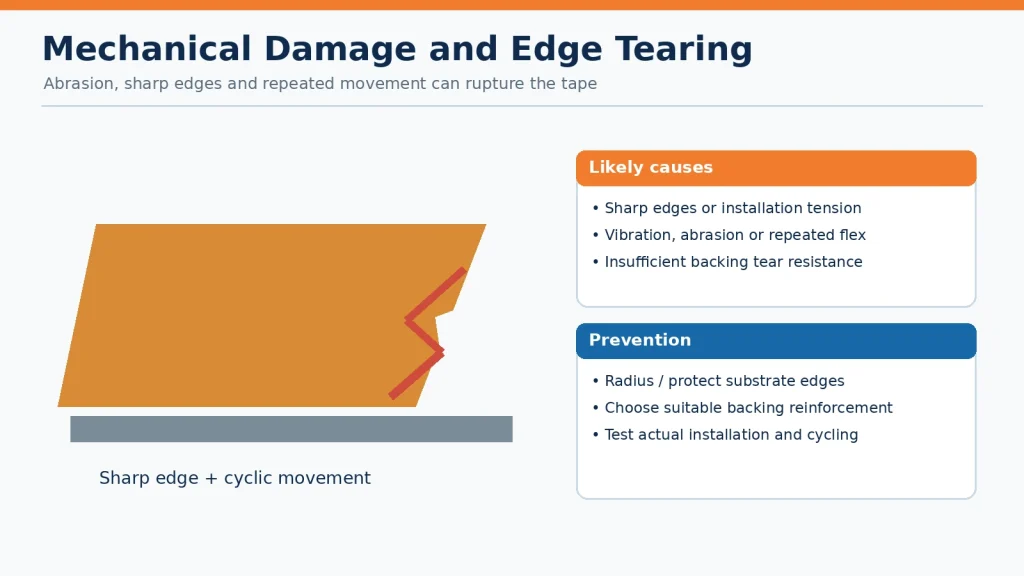
Mechanical damage can occur during installation, processing or service.
It may affect the backing even when the adhesive itself performs adequately.
Typical Symptoms
- Tearing at sharp edges
- Punctures
- Abrasion marks
- Damage around holes or corners
- Cracks after repeated bending
- Failure during tape removal
Common Causes
Sharp substrate edges
Metal edges and corners can concentrate stress.
Excessive installation tension
Stretching a tape during application may create residual stress.
Repeated movement
Vibration or thermal expansion can create abrasion or fatigue.
Insufficient backing strength
A thin film may not provide adequate tear or puncture resistance for a particular design.
Prevention Strategies
- Reduce sharp-edge contact where practical.
- Specify suitable edge radii or protective features.
- Avoid unnecessary stretching during application.
- Select backing thickness and reinforcement according to mechanical needs.
- Evaluate abrasion, puncture and flexural requirements.
- Test the installed construction.
Film-Backed vs Fabric-Reinforced Tapes
Film-backed tapes can provide useful flexibility and conformability.
Fabric-reinforced constructions may offer advantages in certain mechanically demanding applications.
However, the appropriate choice depends on the exact material, weave, coating, adhesive and intended function.
No backing type is universally superior.
9. How to Select the Right Backing and Adhesive
High-temperature tape selection involves two major decisions:
- Backing material
- Adhesive system
Backing Material Comparison
| Backing | Potential Advantages | Selection Considerations |
|---|---|---|
| Polyimide (PI) film | High-temperature capability in suitable grades; thin flexible insulation | Adhesive rating, dielectric needs, dimensional stability |
| PET film | Cost-effective and widely available | Temperature limit, shrinkage, mechanical requirements |
| PTFE film | Chemical resistance and low-friction characteristics | Bonding difficulty, creep and dimensional behavior |
| PTFE-coated fiberglass | Reinforced construction and nonstick surface in suitable grades | Thickness, flexibility, coating integrity and adhesive compatibility |
| Glass cloth | Mechanical reinforcement and selected high-temperature applications | Fraying, thickness, conformability and adhesive system |
Adhesive Chemistry Comparison
| Adhesive System | Potential Strengths | Important Limitations |
|---|---|---|
| Silicone PSA | Useful high-temperature options in suitable formulations | Residue, substrate compatibility, contamination sensitivity |
| Acrylic PSA | Broad formulation flexibility and bonding options | Grade-specific temperature and aging limits |
| Rubber-based PSA | Strong initial tack in selected applications | Often more limited heat and aging resistance, depending on formulation |
| Other specialized systems | Application-specific performance | Availability and verified qualification data required |
A high-temperature backing combined with an unsuitable adhesive may still fail.
Selection Principle
Do not select a tape by backing material alone.
For demanding applications, evaluate backing, adhesive, substrate and service conditions as one system.
10. Testing and Failure Analysis
A useful qualification program should reproduce the conditions that caused or could cause failure.
Step 1: Document the Application
Record:
- Substrate material and surface finish
- Application temperature
- Application pressure
- Bonding dwell time
- Tape dimensions and thickness
- Mechanical loading
- Chemical exposure
- Removal conditions
Step 2: Define the Temperature Profile
Specify:
- Minimum temperature
- Maximum temperature
- Heating and cooling rate
- Exposure duration
- Number of cycles
- Atmosphere, if relevant
Step 3: Measure Initial Properties
Depending on the application, measure:
- Peel adhesion
- Shear adhesion
- Tack
- Backing tensile properties
- Elongation
- Thickness
- Visual appearance
Step 4: Apply Representative Exposure
Test samples using conditions relevant to the actual process or service environment.
Step 5: Re-Evaluate Performance
After exposure, assess:
- Adhesion retention
- Edge lifting
- Cohesive failure
- Adhesive transfer
- Cracking
- Dimensional change
- Clean removal
- Electrical properties, if applicable
Step 6: Identify the Failure Location
Determine whether the failure occurred:
- Between adhesive and substrate
- Within the adhesive
- Between adhesive and backing
- Within the backing
- At another coating or primer interface
This step is essential for selecting corrective action.
Relevant Test Methods
| Test | Relevant Reference | Purpose |
|---|---|---|
| Peel adhesion | ASTM D3330/D3330M | Compare peel adhesion under defined conditions |
| Shear adhesion | ASTM D3654/D3654M | Evaluate shear holding behavior |
| Tensile properties | ASTM D3759/D3759M | Evaluate tape tensile strength and elongation |
| Thermal aging | Application-specific protocol | Evaluate changes after heat exposure |
| Temperature cycling | IEC 60068-2-14, where applicable | Evaluate effects of defined temperature changes |
| Residue inspection | Agreed application-specific method | Evaluate cleanliness after removal |
The standards listed are references for selecting methods, not evidence that any HighTemp Material product has passed a particular test.
Test acceptance criteria must be established for the intended application.
11. Troubleshooting: Match the Symptom to the Correct Action
| Observed Problem | First Checks | Possible Corrective Actions |
|---|---|---|
| Tape lifts during heating | Surface cleanliness, adhesive compatibility, temperature | Improve preparation, evaluate different adhesive |
| Residue after removal | Heat duration, removal conditions, adhesive cohesion | Qualify clean-removal construction |
| Adhesive splits | Cohesive strength, shear load, aging | Adjust adhesive construction or loading |
| Backing cracks | Temperature exposure, aging, mechanical stress | Review backing grade and geometry |
| Tape swells | Chemical identity, concentration, temperature | Select compatible complete construction |
| Tape tears at edge | Edge radius, installation tension, backing strength | Protect edge, adjust thickness or reinforcement |
Changing to a tape with a higher advertised temperature rating is not necessarily the correct response.
The replacement must address the actual failure mechanism.
12. Application Examples
PCB and SMT Masking
Temporary masking tapes may experience elevated temperatures during manufacturing.
Important requirements include:
- Adequate adhesion during processing
- Dimensional stability
- Controlled removal
- Low unacceptable residue
- Compatibility with PCB surface finishes
Powder Coating and Surface Finishing
Masking tapes must remain in place during the relevant heating process.
After processing, removal quality and surface cleanliness may be critical.
Battery and Power Electronics
Adhesive-backed insulation components may experience thermal cycling, mechanical stress and long-term service conditions.
Important criteria include:
- Electrical insulation
- Adhesion retention
- Dimensional stability
- Resistance to edge lifting
- Environmental durability
Industrial Equipment
Equipment insulation and protective tapes may encounter elevated temperature, vibration and chemical exposure.
The correct selection depends on the complete service environment.
13. RFQ Checklist for High-Temperature Adhesive Tapes
To obtain a meaningful material recommendation, provide:
| Requirement | Information Needed |
|---|---|
| Application | SMT masking, insulation, powder coating, battery or industrial |
| Function | Temporary masking or permanent bonding |
| Substrate | Aluminum, stainless steel, PCB, glass, plastic or coated surface |
| Temperature | Continuous and peak temperature |
| Exposure duration | Seconds, minutes, hours or long-term |
| Thermal cycles | Temperature range and number of cycles |
| Removal | Required or not; temperature and method |
| Residue tolerance | Visual, functional or cleanliness criteria |
| Chemicals | Solvents, oils, cleaners and concentrations |
| Mechanical stress | Peel, shear, bending, vibration or abrasion |
| Tape construction | Preferred backing and adhesive |
| Dimensions | Width, length, thickness and tolerance |
| Converting | Roll, slit roll, sheet or die-cut part |
| Documentation | TDS, test reports, compliance requirements |
| Quantity | Samples and estimated production demand |
If an existing tape has failed, include photographs, process conditions and a description of the failure location.
These details are often more useful than requesting a tape with a higher temperature rating.
14. High-Temperature Tape and Custom Converting Support
HighTemp Material supplies high-temperature polymer films, industrial adhesive tapes and precision-converted insulation materials.
Relevant product and material categories include:
- Polyimide film tapes
- PTFE-based adhesive tapes
- PET-based adhesive materials
- Selected reinforced and specialty tapes
- Custom die-cut insulation components
Depending on the application and available material grades, converting requirements may include:
For material selection, we can discuss the intended temperature profile, substrate, adhesive construction, dimensions and available technical documentation.
Request Tape Selection Support
Are you experiencing tape lifting, adhesive residue, cracking or failure during high-temperature processing?
Send us:
- Your current tape type
- Substrate material
- Temperature and exposure time
- Description or photos of the failure
- Required tape dimensions
- Estimated quantity
Contact HighTemp Material to discuss suitable high-temperature adhesive tape and custom converting options.
Frequently Asked Questions
Why does high-temperature tape leave residue?
Residue may result from adhesive aging, cohesive failure, excessive bonding to the substrate or unsuitable removal conditions. The exact cause should be established through testing.
Why does polyimide tape lift during heating?
Possible causes include contamination, low surface energy, inadequate application pressure, thermal expansion mismatch or an unsuitable adhesive formulation.
What is the difference between adhesive failure and cohesive failure?
Adhesive failure occurs at an interface. Cohesive failure occurs within the adhesive layer itself.
Is silicone adhesive always better for high temperatures?
No. Silicone adhesives include formulations suitable for demanding temperatures, but their performance depends on the grade, substrate, exposure and required removal behavior.
Can PTFE adhesive tape fail under heat?
Yes. PTFE backing performance does not establish the performance of the adhesive or other layers. The complete tape construction must be evaluated.
Does higher peel strength mean better tape performance?
Not necessarily. Strong initial adhesion may be undesirable for clean-removal masking, and it does not guarantee thermal aging or shear performance.
How can adhesive residue be prevented?
Use a tape qualified for the actual temperature profile, substrate and removal process. Evaluate residue after representative heat exposure rather than relying only on room-temperature data.
Which test is best for high-temperature adhesive tape?
There is no single universal test. Peel, shear, tensile, thermal aging, cycling and removal tests may all be relevant depending on the application.
Can a tape pass a short peak-temperature test but fail in continuous service?
Yes. Short-term exposure and prolonged heating can produce different effects. Continuous and peak temperature claims should be assessed separately.
Should the backing and adhesive be tested separately?
Individual material data can help, but the complete tape construction should also be qualified under representative conditions.
Conclusion
High-temperature adhesive tape failures are not caused by temperature alone.
Adhesion loss, residue, cohesive splitting, thermal degradation, chemical attack and mechanical damage can arise from different combinations of material selection, processing conditions, substrate characteristics and mechanical stress.
Successful troubleshooting begins by identifying the actual failure mechanism.
Engineers should then select the backing and adhesive as a complete construction, compare test data under relevant conditions and validate performance in the intended application.
For PCB/SMT masking, battery insulation, powder coating and industrial applications, this approach can reduce rework and improve material-selection confidence.
Contact HighTemp Material for high-temperature adhesive tape and custom converting discussions.
Engineering disclaimer: The mechanisms and recommendations in this guide are general engineering information. They do not represent verified performance claims for a particular tape grade. Temperature limits, test results, certifications and converting capabilities must be confirmed for the exact material and application.