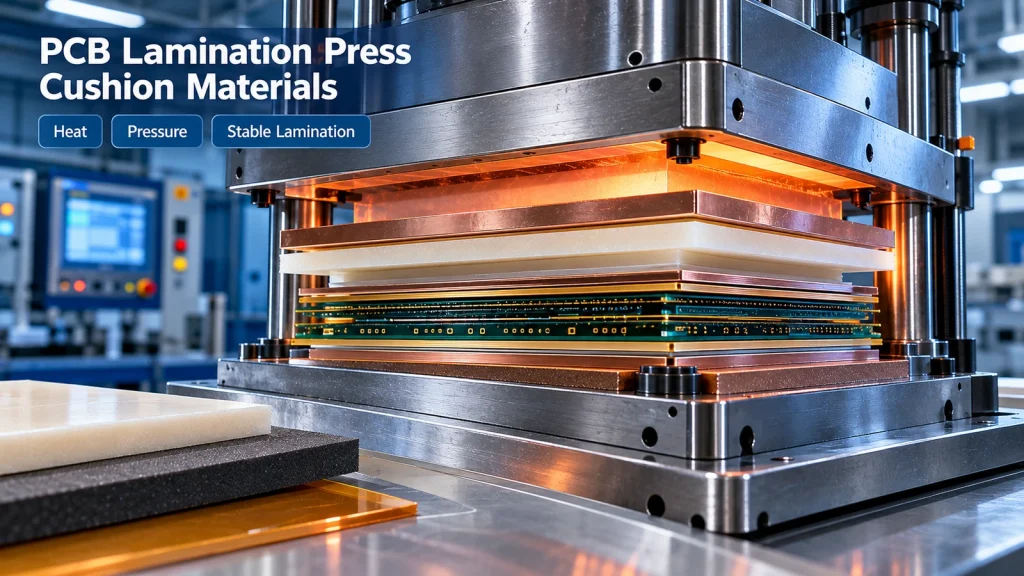
In multilayer printed circuit board (PCB) manufacturing, a successful lamination cycle depends on more than the resin system, press temperature, and nominal applied pressure. The condition of the press tooling and the materials used within the lamination stack can also influence contact uniformity, heat transfer, dimensional stability, and process repeatability.
PCB lamination press cushion materials are engineered process layers used to accommodate limited variations in the pressing system and help manage the mechanical contact conditions experienced by the laminate assembly.
An unsuitable or deteriorated cushion can contribute to uneven pressure transfer, local surface impressions, inconsistent resin flow, and variable results between press cycles. However, these symptoms can also arise from platen condition, stack design, resin behavior, heating profiles, or process control. Cushion performance should therefore be evaluated as part of the complete lamination system.
This engineering guide explains how press cushion materials work, how common constructions differ, which properties matter most, how to investigate failures, and how to establish qualification and maintenance requirements for reliable PCB manufacturing.
1. What Are PCB Lamination Press Cushion Materials?
A press cushion material is a compressible or conformable layer positioned within a lamination press assembly to manage mechanical contact between the tooling and the workpiece stack.
Depending on the press configuration, a cushion layer may help accommodate limited thickness variation, tooling irregularities, or changes in contact geometry during heating and loading.
Its effectiveness depends on the material construction, compressive response, thickness, thermal behavior, condition after repeated cycles, and position in the stack.
1.1 Cushion materials versus release films
A cushion pad and a release film perform different primary functions.
A press cushion is selected primarily for its mechanical response under load and its suitability for the press environment.
A release film is selected primarily for its ability to control adhesion or separation at a defined interface.
A thermal barrier or insulation layer is selected for its effect on heat transfer or electrical insulation, depending on the application.
Some engineered constructions combine multiple functions, but these functions must be demonstrated rather than assumed.
For example, PTFE may be useful as a low-friction or release-facing component in a composite construction, but a thin PTFE film should not automatically be classified as a suitable pressure-distribution cushion.
1.2 Where are cushion materials installed?
The position of a cushion depends on the press design and process requirements. It may be located between tooling components, adjacent to caul plates, or in another defined location within the pressing assembly.
A simplified conceptual stack might contain:
- Upper heated platen or press tooling.
- Cushion or pressure-distribution layer.
- Caul plate or other tooling layer.
- PCB laminate and prepreg assembly.
- Additional process or separation layers.
- Lower tooling and platen.
This is not a universal stack-up. Actual layer positions, symmetry, and tooling arrangements must follow the qualified process design and equipment manufacturer’s requirements.
2. How Press Cushion Materials Work
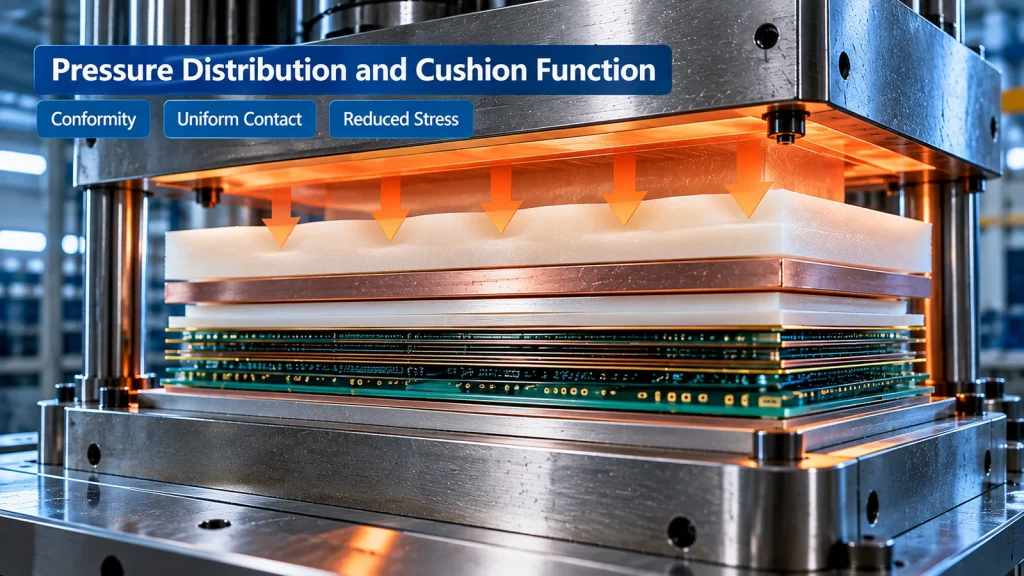
2.1 Pressure distribution and conformity
When a press applies force, the resulting local contact pressure is affected by the geometry and mechanical response of the complete stack.
A compliant cushion may accommodate limited variations in thickness or contact geometry. This can help reduce local concentration of contact stresses under suitable conditions.
However, a cushion does not guarantee uniform pressure. Excessive compliance, inappropriate thickness, or uneven material condition can introduce other problems.
The objective is not simply to select the softest material. It is to obtain a controlled compressive response appropriate for the equipment, laminate, and process cycle.
2.2 Compression and elastic recovery
A cushion deforms under load. After unloading, some or all of that deformation may recover.
Three concepts should be distinguished:
Compressibility describes deformation under a defined load.
Recovery describes the material’s return toward its previous thickness after unloading.
Compression set describes retained deformation after a specified compression and recovery procedure.
These properties depend on test conditions. Measurements obtained at room temperature cannot automatically predict behavior during a heated lamination cycle.
For repeated-use applications, recovery after thermal and mechanical cycling may be more informative than initial compressibility alone.
2.3 Thermal contact and heat transfer
Cushion layers can influence the thermal behavior of the press stack.
Depending on their composition and thickness, they may affect thermal resistance, contact conditions, heat-up rate, and temperature distribution.
A material that provides useful mechanical compliance may also alter heat transfer. These effects must be considered together.
A cushion should not be described as improving temperature uniformity without appropriate process evidence.
2.4 Surface protection and tooling interaction
A properly specified cushion may help reduce certain local contact irregularities, but it can also transfer defects if its surface is damaged or contaminated.
Surface scratches, particles, embedded debris, local hard spots, and thickness variation can affect the contact condition.
The surface condition of the cushion, caul plates, and adjacent process layers should therefore be included in routine inspection.
3. Types of PCB Press Cushion Materials
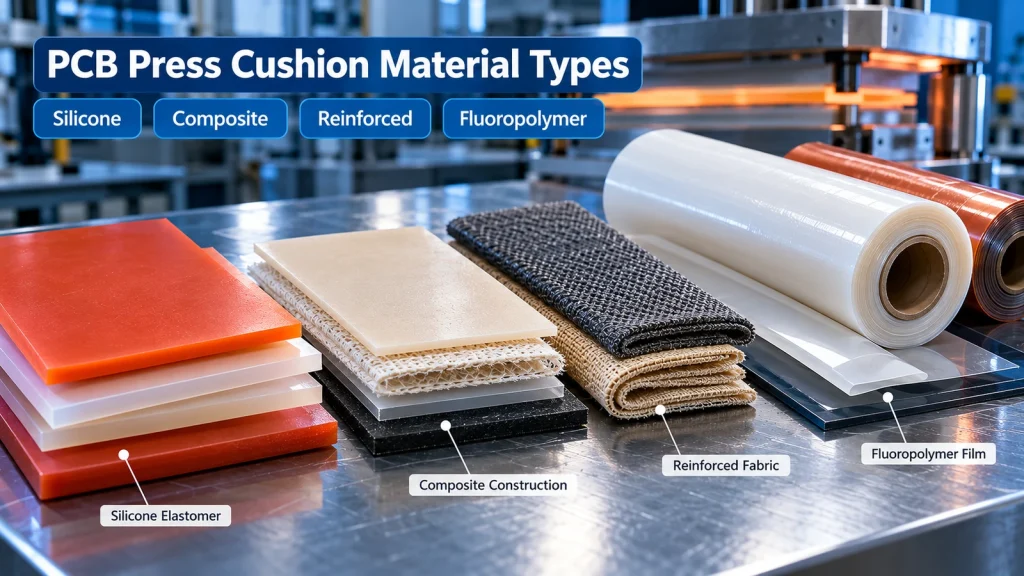
Several material families and constructions may be considered, depending on the press configuration and required performance.
The material family alone is not enough to establish suitability. Composite architecture, reinforcement, coatings, processing history, and grade-specific properties may be decisive.
3.1 Silicone rubber-based cushions
Silicone elastomers can provide compressibility and recovery characteristics that make them candidates for engineered cushion applications.
Important evaluation factors include hardness, compressive response, compression set, thermal aging, surface condition, and potential contamination.
The presence of silicone may be restricted in certain manufacturing environments. Where contamination sensitivity is significant, evaluate the complete material construction and any applicable process restrictions.
3.2 Fiber-reinforced and fabric-based constructions
Engineered textile or fiber-reinforced cushion constructions may be designed to balance compliance, dimensional stability, and handling.
Their behavior depends on fiber composition, weave or reinforcement architecture, binders, and overall construction.
Potential concerns include fraying, particle shedding, permanent compaction, and changes in performance after repeated pressing.
3.3 Composite cushion pads
Multilayer composite constructions may combine compliant layers with reinforcing or protective components.
The goal may be to balance pressure response, durability, dimensional stability, and surface characteristics.
The performance of the complete construction must be evaluated. The properties of a single constituent material cannot be used as a substitute for composite qualification.
3.4 Fluoropolymer and polyimide components
PTFE and polyimide are important high-performance polymer families, but their presence in a pressing assembly does not automatically make them cushion materials.
PTFE may be considered for release-facing or low-friction functions. Polyimide may be considered where particular thermal and mechanical characteristics are required.
Whether either material belongs in a cushion construction depends on the full design and validated application.
3.5 Material comparison table
| Material or construction | Potential engineering benefit | Main qualification concern | Selection guidance |
|---|---|---|---|
| Silicone elastomer-based cushion | Compliant mechanical response | Compression set, aging, contamination and grade-specific thermal behavior | Evaluate under actual load and thermal cycling |
| Reinforced fabric cushion | Engineered balance of compliance and reinforcement | Compaction, fraying, particle generation and construction variation | Assess recovery, cleanliness and dimensional consistency |
| Multilayer composite cushion | Ability to combine different functional layers | Interlayer integrity, delamination and repeatability | Qualify the complete composite |
| PTFE-containing construction | Low-friction or release-facing functionality | Insufficient cushioning, deformation or interface incompatibility | Treat as a functional component unless cushioning is demonstrated |
| PI-containing construction | Potential thermal and mechanical functionality | Limited conformity of some constructions and grade-specific behavior | Verify the intended function and finished construction |
| Specialty engineered press pad | Application-specific mechanical and thermal design | Documentation, availability and process-specific qualification | Compare against a defined baseline and acceptance criteria |
Engineering note: This table describes general material considerations, not confirmed HighTemp Material product grades or validated performance claims.
4. Key Engineering Selection Factors
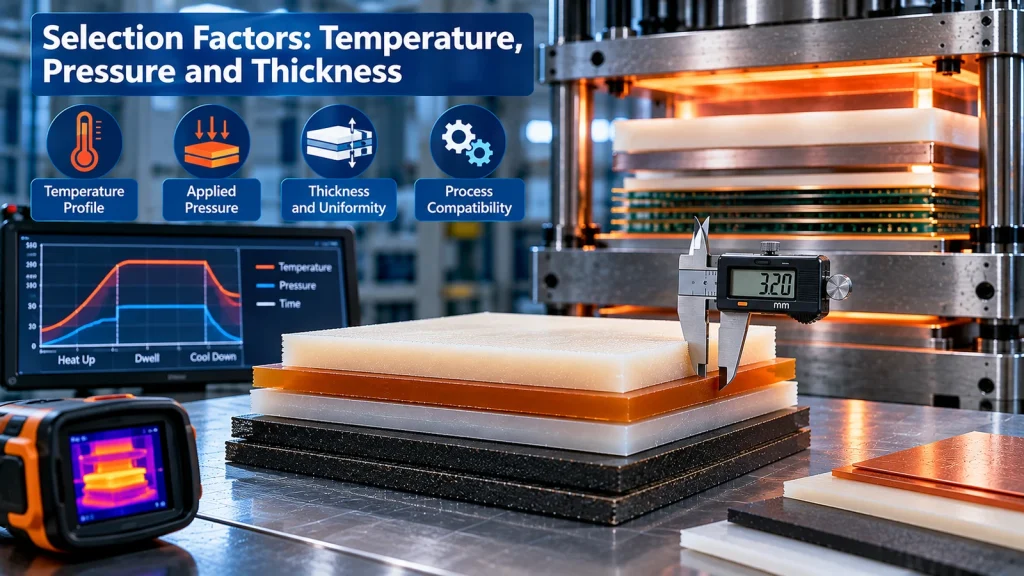
4.1 Actual temperature-time profile
The press controller setting does not necessarily represent the temperature experienced by every layer in the stack.
Specify the relevant temperature profile, including peak temperature, exposure duration, heating and cooling stages, and repeated-cycle conditions.
For a composite cushion, consider whether the elastomer, reinforcement, coating, and adhesive or binder have different thermal limitations.
4.2 Applied pressure and loading profile
The nominal press pressure must be interpreted in the context of the equipment and stack geometry.
Relevant information includes:
- Applied force or pressure and the basis on which it is reported.
- Contact area and panel size.
- Loading and unloading sequence.
- Time under pressure.
- Number of repeated cycles.
- Local thickness differences or tooling irregularities.
Cushion performance should be evaluated using representative loading conditions.
4.3 Compressibility under operating conditions
A cushion should deform sufficiently to perform its intended function without causing unacceptable stack displacement or instability.
Ask for compressive stress-strain data when available, and check the temperature and loading conditions used to obtain it.
Avoid comparing compressibility percentages without checking their measurement methods.
4.4 Compression recovery and permanent deformation
For reusable cushions, changes in recovery may indicate deterioration.
A material can appear acceptable when new but progressively lose thickness or compliance after repeated use.
Qualification should examine the retained thickness, recovery behavior, and relevant surface changes after representative cycles.
4.5 Thickness and thickness uniformity
Cushion thickness can influence contact behavior, heat transfer, stack height, and handling.
Define the nominal thickness, tolerance, measurement method, and acceptable variation across the sheet.
A thicker cushion is not automatically better. The correct thickness must be determined in relation to the press and laminate design.
4.6 Thermal conductivity and thermal resistance
A cushion layer may affect heat flow between tooling and the laminate.
When temperature uniformity or cycle time is critical, thermal properties should be considered alongside mechanical properties.
A material with favorable compressibility may require adjustments to the thermal process, and any changes should be validated.
4.7 Surface cleanliness and compatibility
Inspect potential sources of particles, residue, volatile components, coating transfer, or contamination.
Where electrical reliability or sensitive bonding interfaces are involved, cleanliness requirements should be defined according to the product and manufacturing risk.
4.8 Durability and total operating cost
Purchase price per sheet does not describe the complete cost of a cushion material.
Consider:
- Qualified number of press cycles.
- Inspection and replacement frequency.
- Scrap and rework risk.
- Labor required for handling and maintenance.
- Availability and lot consistency.
- Process downtime caused by material changes.
Service life should be established from actual operating evidence, not assumed from generic material descriptions.
5. Typical Industrial Applications
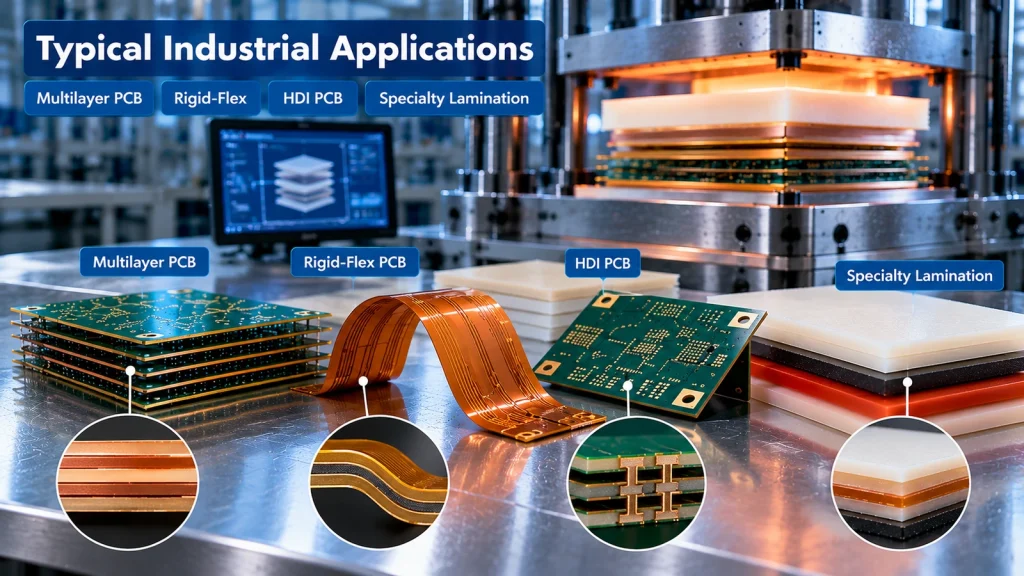
5.1 Multilayer rigid PCB lamination
Multilayer PCB pressing requires coordinated control of resin flow, temperature, pressure, and stack geometry.
A cushion material may be used to manage the mechanical contact conditions within the press assembly.
Important qualification outcomes include laminate thickness consistency, acceptable surface condition, and repeatable performance across the panel and between press cycles.
5.2 HDI and fine-feature PCB manufacturing
High-density interconnect manufacturing can involve demanding dimensional and quality requirements.
Cushion selection should be considered alongside the complete press stack and process-control strategy.
A change in cushion material should trigger an assessment of whether the qualified lamination conditions remain appropriate.
5.3 Rigid-flex PCB assemblies
Rigid-flex constructions may contain regions with different local thicknesses and mechanical responses.
These differences can complicate contact and pressure distribution.
A cushion may be one part of the solution, but the complete tooling arrangement, local support, stack design, and resin system must be evaluated.
5.4 Other precision lamination processes
Related cushioning principles may be relevant to certain electronic-material, insulating laminate, and composite pressing operations.
However, successful use in PCB manufacturing does not automatically qualify a material for semiconductor, battery, or other manufacturing applications.
Each process requires its own compatibility and performance assessment.
6. Common Selection Mistakes
Mistake 1: Choosing a cushion only by material name
Two silicone-based or composite cushions may behave differently because of hardness, reinforcement, fillers, thickness, and manufacturing methods.
Prevention: Specify the finished construction and critical performance requirements.
Mistake 2: Assuming greater softness is always better
Excessive compliance may produce unwanted displacement or an unstable pressing arrangement.
Prevention: Evaluate the compressive response over the actual operating load range.
Mistake 3: Ignoring thermal effects
Mechanical properties can change during heating, prolonged loading, and cooling.
Prevention: Test under representative thermal and mechanical conditions.
Mistake 4: Treating a release film as a cushion pad
A thin release film may not provide the required mechanical compliance.
Prevention: Separate release, cushioning, and thermal functions in the engineering specification.
Mistake 5: Ignoring cumulative compression
Repeated cycles may change cushion thickness and recovery.
Prevention: Establish periodic measurements and condition-based replacement criteria.
Mistake 6: Replacing the cushion without investigating defects
Surface marks or thickness variation may also originate from tooling, resin, or process settings.
Prevention: Use a controlled root-cause investigation.
Mistake 7: Approving a single sample without production controls
A successful trial does not guarantee lot-to-lot consistency.
Prevention: Define incoming inspection, traceability, supplier change control, and periodic verification.
7. Common Failure Modes and Prevention
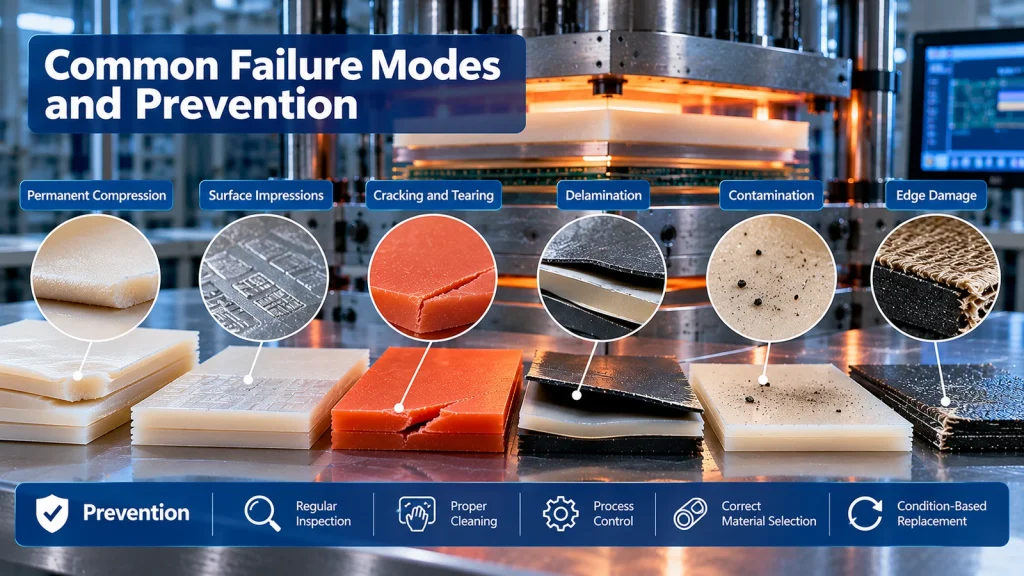
| Failure or symptom | Potential contributing factors | Investigation and prevention |
|---|---|---|
| Permanent thickness loss | Repeated compression, thermal aging or unsuitable construction | Monitor thickness and recovery; compare with approved baseline |
| Uneven pressure transfer | Local cushion damage, tooling variation, misalignment or stack geometry | Inspect cushion and tooling; review press conditions |
| Surface impressions | Particles, embedded debris, damaged cushion surface or adjacent tooling | Clean and inspect contact surfaces; isolate defect origin |
| Cracking or tearing | Aging, mechanical stress, edge damage or handling | Inspect material integrity and handling procedure |
| Delamination of composite pad | Interlayer incompatibility, repeated stress or thermal exposure | Inspect bonding integrity and validate the full construction |
| Curl or distortion | Uneven exposure, residual stress or material changes | Check flatness, dimensions and process history |
| Contamination | Particle shedding, residue, cleaning incompatibility or handling | Define cleanliness controls and compatible cleaning procedures |
| Inconsistent press results | Cushion deterioration, lot variation or process drift | Compare material records, press settings and laminate inspection results |
The same defect can have multiple causes. Use comparative trials, equipment checks, and process records before concluding that the cushion material is responsible.
8. Maintenance and Replacement Strategy
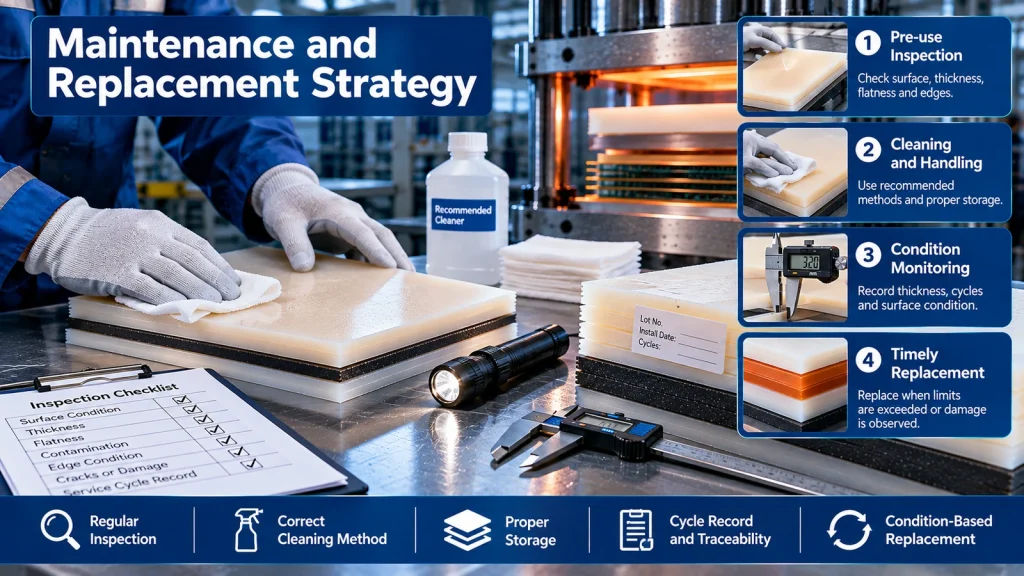
A documented maintenance program helps detect deterioration before it causes unacceptable process variation.
8.1 Pre-use inspection
Before installation, inspect the cushion for visible damage, contamination, abnormal thickness variation, curling, tears, and signs of permanent deformation.
Confirm that the correct material identification and approved dimensions are being used.
8.2 Cleaning and handling
Follow the material supplier’s documented cleaning instructions.
Do not assume that solvents, abrasive cleaning methods, or aggressive mechanical scraping are compatible with the cushion construction.
Use appropriate handling and storage practices to prevent contamination, bending damage, and edge deterioration.
8.3 Condition monitoring
A condition-monitoring program may record:
- Number of press cycles.
- Relevant temperature and pressure history.
- Thickness at defined measurement locations.
- Visible surface condition.
- Compression recovery where practical.
- Defects or unusual process observations.
Record the material lot and installation date to support traceability.
8.4 When should a cushion be replaced?
Replacement criteria should be based on the qualified material and process, not an arbitrary universal cycle count.
Possible triggers include:
- Thickness or recovery outside the approved limits.
- Cracking, tearing, delamination, or other structural damage.
- Unacceptable surface contamination or damage.
- Evidence of deterioration affecting process repeatability.
- Completion of a validated maximum service interval, where one has been established.
8.5 Storage recommendations
Store materials according to supplier instructions.
Protect them from contamination, excessive mechanical deformation, and environmental exposure outside the documented storage conditions.
Avoid inventing universal shelf-life or storage-temperature limits without grade-specific evidence.
9. Testing and Qualification
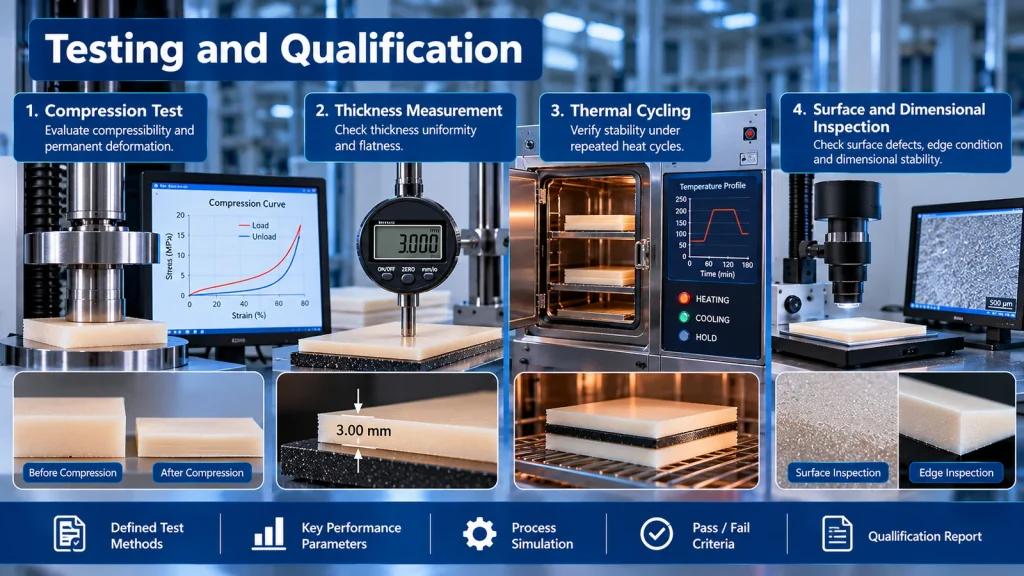
9.1 Documentation review
Request the exact material identification and relevant technical documentation.
Depending on the construction, useful information may include thickness tolerance, compressive response, recovery, thermal behavior, surface characteristics, and recommended handling.
A test report should identify the test method and conditions. General polymer data should not be substituted for the finished cushion construction.
9.2 Thickness and dimensional inspection
Measure thickness at defined locations using a suitable instrument and method.
Record the sample conditioning, applied measurement force where relevant, and the measurement positions.
Compare variation within the sheet and between lots against agreed requirements.
9.3 Compression testing
Compression testing should characterize the cushion under relevant loading conditions.
Possible evaluations include compressive stress-strain response, deformation under a specified load, and recovery after unloading.
Where appropriate, investigate the effect of temperature and repeated cycles.
For elastomeric materials, methods such as ASTM D395 may be relevant to certain compression-set evaluations, but applicability to the actual finished cushion construction must be confirmed. It should not be assumed to represent a complete PCB lamination qualification.
9.4 Thermal aging and repeated-cycle testing
Expose samples to representative thermal and mechanical cycles.
Inspect for permanent deformation, cracking, changes in compressibility, surface damage, and loss of functional integrity.
A simple oven-aging test may support preliminary screening but does not fully reproduce simultaneous pressure, contact, and thermal cycling inside a production press.
9.5 Pressure distribution evaluation
Where process risk justifies it, evaluate the pressure distribution or contact condition using a validated method appropriate to the press.
Pressure-sensitive media, instrumented tooling, or other measurement approaches may be useful, but each has its own limitations.
Measurements should be interpreted alongside tooling geometry and process conditions.
9.6 Production trial and acceptance
Compare the candidate cushion with an approved baseline under controlled conditions.
Record:
- Material construction, dimensions, and lot.
- Press equipment and stack arrangement.
- Temperature, pressure, time, and cooling profile.
- Initial and post-cycle material condition.
- Laminate inspection results.
- Deviations and corrective actions.
- Final approval or rejection decision.
Acceptance criteria must be established from product requirements and validated process capability.
10. Engineering Selection Workflow
Step 1: Define the cushion’s role
Identify whether the material is intended for pressure conformity, contact management, surface protection, or another specific function.
Step 2: Document the press environment
Record the equipment configuration, stack design, actual temperature profile, loading conditions, and expected usage pattern.
Step 3: Establish critical properties
Define thickness, tolerance, compressibility, recovery, dimensional stability, cleanliness, and other mandatory requirements.
Step 4: Screen candidate constructions
Compare available material families and complete constructions. Identify missing data and supplier confirmation requirements.
Step 5: Conduct laboratory and process trials
Test candidate materials under representative conditions and compare them with a qualified baseline.
Step 6: Evaluate repeated-cycle behavior
Assess whether properties remain acceptable over the intended use period.
Step 7: Approve the specification
Document the approved construction, dimensions, quality requirements, test methods, and change-control conditions.
Step 8: Implement maintenance controls
Establish inspection intervals, recordkeeping, replacement criteria, and procedures for handling unexpected deterioration.
11. RFQ Checklist for PCB Press Cushion Materials
A useful RFQ should describe both the material requirements and the intended press process.
| Information required | Details to provide |
|---|---|
| Application | Multilayer rigid PCB, HDI, rigid-flex or another defined process |
| Cushion function | Pressure conformity, contact management or another required function |
| Existing material | Current cushion type, construction, and available specification |
| Material preference | Silicone, reinforced fabric, composite or supplier-recommended alternative |
| Temperature | Peak temperature, exposure time, heating and cooling profile |
| Pressure | Applied load or pressure, reporting basis, dwell time and cycle sequence |
| Thickness | Nominal thickness, tolerance and measurement method |
| Dimensions | Sheet size, usable area, edge requirements and drawings |
| Mechanical requirements | Compressibility, recovery, compression set and relevant test conditions |
| Thermal requirements | Thermal behavior and any heat-transfer constraints |
| Electrical requirements | Applicable electrical insulation or dielectric requirements, if the layer has an electrical function |
| Cleanliness | Particle, residue, contamination and handling restrictions |
| Service life | Intended reuse, inspection criteria and expected operating conditions |
| Quality documents | TDS, applicable test reports, traceability and required standards |
| Commercial details | Sample quantity, forecast consumption, order quantity and destination |
If the customer is replacing an existing cushion, a reference sample, material drawing, and description of the current problem can significantly improve technical evaluation.
12. Frequently Asked Questions
1. What is a PCB lamination press cushion material?
It is a process material used within a PCB pressing assembly to manage mechanical contact and accommodate certain variations in the tooling or stack. Its required properties depend on the equipment, laminate construction, and process conditions.
2. Why is cushioning needed during PCB lamination?
A cushion may help manage local contact differences and mechanical loading. However, it cannot compensate for every tooling or process problem. The full pressing system must be designed and validated appropriately.
3. Are silicone rubber cushions better than composite cushions?
Neither construction is universally superior. Silicone elastomer-based and composite materials may offer different combinations of compliance, recovery, dimensional stability, durability, and contamination characteristics. Selection requires application-specific testing.
4. How does cushion thickness affect PCB lamination?
Thickness can influence compressive behavior, contact conditions, stack height, and thermal resistance. A thicker pad is not automatically more suitable. The correct specification depends on the press and process design.
5. Can PCB press cushion pads be reused?
Some constructions may be designed for repeated use, but reuse must be supported by the supplier’s guidance and process qualification. Inspect material condition and monitor relevant properties before continued use.
6. What causes permanent compression in a cushion pad?
Repeated loading, elevated-temperature exposure, material aging, and unsuitable construction may contribute to permanent deformation. The mechanism should be evaluated under the actual operating conditions.
7. When should a press cushion be replaced?
Replace it when qualified dimensional, mechanical, cleanliness, or structural limits are exceeded, or when it reaches a validated service interval. There is no universal replacement cycle count applicable to every material and process.
8. How should cushion materials be tested before production?
Review grade-specific documentation, inspect dimensions, evaluate compressive behavior and recovery, assess thermal cycling, and perform controlled press trials. Acceptance criteria should be agreed before testing.
9. Can a release film replace a press cushion?
Not automatically. A release film primarily manages adhesion and separation, whereas a cushion must provide a defined mechanical response under load. A material intended for both functions requires evidence for both.
10. What information should be provided when requesting a PCB press cushion quotation?
Provide the press application, material preference, temperature and pressure profiles, thickness, dimensions, drawings, electrical or cleanliness requirements where relevant, testing standards, sample needs, and estimated purchase quantity.
13. Request a PCB Press Cushion Material Review or Quotation
A reliable press cushion specification should address the complete lamination environment—not just the polymer type or nominal sheet thickness.
HighTemp Material works with high-temperature polymer films, electrical insulation materials, and converting-related requirements. Availability and suitability of a particular PCB press cushion construction must be confirmed before any product recommendation or quotation is finalized.
If you are evaluating press cushion materials, replacing an existing pad, or investigating lamination consistency, please share:
- PCB application and current press stack configuration.
- Existing cushion material or reference sample.
- Peak temperature, pressure, dwell time, and expected reuse.
- Required thickness, tolerance, sheet dimensions, and drawings.
- Compression, recovery, thermal, or electrical requirements.
- Surface cleanliness and contamination restrictions.
- Applicable testing standards and acceptance criteria.
- Sample requirements, estimated order quantity, and annual consumption.
Contact HighTemp Material to discuss your application and request a technical review or quotation.
Website: https://www.hightempmaterial.com/
Technical disclaimer: Material descriptions in this article are general engineering guidance. Actual product availability, grade specifications, test results, service life, and application suitability require supplier confirmation and process-specific validation.